

Cold storage facilities play a vital role in industries such as food processing, pharmaceuticals, agriculture, hospitality, and logistics. These facilities are designed to maintain controlled temperatures that preserve products and ensure quality throughout storage and transportation. To achieve reliable temperature control and energy efficiency, the building materials used in cold rooms and refrigerated warehouses must meet high-performance standards. One of the most effective solutions available today is insulated sandwich panels.
Insulated sandwich panels have become a preferred choice for cold storage construction because they provide excellent thermal insulation, structural strength, durability, and quick installation. These panels help businesses reduce operational costs while ensuring stable temperature conditions inside the facility. As the demand for modern refrigeration and cold chain infrastructure continues to grow, insulated sandwich panels are becoming an essential component in cold storage development.
What Are Insulated Sandwich Panels?
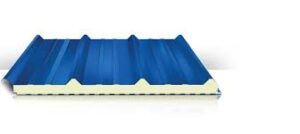
Insulated sandwich panels are composite building materials made with two outer metal sheets and an insulating core placed between them. The outer layers are usually manufactured from galvanized steel or aluminum, while the insulating core can consist of materials such as polyurethane (PU), polyisocyanurate (PIR), or mineral wool.
The layered design of these panels creates a highly effective thermal barrier that minimizes heat transfer between the inside and outside environment. Because of their insulation capabilities and structural performance, sandwich panels are widely used in cold rooms, refrigerated warehouses, food processing plants, and temperature-controlled logistics centers.
Excellent Thermal Insulation Performance
One of the primary reasons insulated sandwich panels are ideal for cold storage facilities is their outstanding thermal insulation. Maintaining low temperatures inside cold rooms requires materials that can prevent heat infiltration from the external environment. Poor insulation can lead to temperature fluctuations, increased energy consumption, and product spoilage.
Sandwich panels with PU or PIR insulation cores provide high thermal resistance, helping cold storage facilities maintain consistent temperatures efficiently. These panels reduce the workload on refrigeration systems, which lowers electricity consumption and operating expenses.
In industries where temperature stability is critical, such as frozen food storage or pharmaceutical preservation, insulated sandwich panels help ensure product integrity and compliance with safety regulations.
Energy Efficiency and Cost Savings
Energy consumption is one of the biggest operational expenses for cold storage facilities. Refrigeration systems run continuously to maintain the required temperatures, making energy-efficient construction essential for reducing long-term costs.
Insulated sandwich panels contribute significantly to energy savings by minimizing thermal leakage. Their airtight design prevents warm air from entering the facility and reduces the amount of energy required to keep the storage area cool.
Over time, businesses can experience substantial reductions in utility bills due to improved insulation performance. This makes sandwich panels a cost-effective investment for both small cold rooms and large industrial refrigeration facilities.
In addition to lower energy costs, these panels also reduce maintenance expenses because refrigeration systems operate more efficiently with less strain.
Fast and Efficient Installation
Construction speed is another major advantage of insulated sandwich panels. Traditional building materials often require lengthy installation processes, which can delay project completion and increase labor costs.
Sandwich panels are prefabricated and designed for easy assembly, allowing construction teams to install them quickly and efficiently. Their lightweight structure simplifies transportation and handling on-site, reducing installation time significantly.
For businesses planning new cold storage projects or expanding existing facilities, faster construction means quicker operational readiness and reduced downtime. This is especially valuable in industries where storage demand is growing rapidly and project timelines are critical.
Hygienic and Easy-to-Clean Surfaces
Cold storage facilities, especially those used for food and pharmaceutical products, must maintain strict hygiene standards. Insulated sandwich panels provide smooth, non-porous surfaces that are easy to clean and sanitize.
The metal surfaces resist moisture accumulation and bacterial growth, helping maintain a hygienic environment inside the facility. This is essential for meeting food safety regulations and industry compliance standards.
Regular cleaning and maintenance become easier because the panels do not absorb contaminants or develop mold easily. Their clean appearance also supports professional facility management and operational efficiency.
Durability and Long Service Life
Cold storage environments expose building materials to moisture, temperature fluctuations, and heavy operational use. Insulated sandwich panels are designed to withstand these challenging conditions while maintaining structural integrity.
The outer metal layers provide strong resistance against corrosion, impact, and environmental damage. High-quality panels are manufactured with protective coatings that enhance durability and extend service life.
Because of their robust construction, sandwich panels require minimal maintenance compared to conventional building materials. This durability helps businesses avoid frequent repairs and replacement costs, making them a reliable long-term solution for cold storage infrastructure.
Fire Safety and Structural Reliability
Modern insulated sandwich panels are manufactured with advanced insulation materials that offer improved fire resistance and safety performance. PIR-core panels, in particular, are known for their enhanced fire-retardant properties compared to traditional insulation materials.
Fire safety is an important consideration for industrial facilities, including refrigerated warehouses and food processing units. Choosing high-quality insulated panels helps improve overall building safety while meeting industry standards and regulations.
In addition to fire performance, sandwich panels provide structural stability and strength. They can support large-span cold storage designs without compromising insulation efficiency or durability.
Versatile Applications in Cold Storage
Insulated sandwich panels are suitable for a wide range of cold storage applications, including:
- Refrigerated warehouses
- Frozen food storage facilities
- Pharmaceutical cold rooms
- Dairy processing plants
- Meat and seafood processing units
- Agricultural storage facilities
- Distribution and logistics centers
Their flexibility allows businesses to customize facility layouts according to operational requirements. Panels are available in different thicknesses and insulation types to accommodate varying temperature needs.
Environmentally Friendly Construction Solution
Sustainability has become an important priority in modern industrial construction. Insulated sandwich panels support environmentally friendly building practices by improving energy efficiency and reducing carbon emissions.
Lower energy consumption means reduced environmental impact over the lifetime of the facility. Additionally, many sandwich panels are manufactured using recyclable materials, supporting sustainable construction goals.
Businesses investing in eco-friendly cold storage infrastructure can benefit from both operational savings and improved environmental performance.
Conclusion
Insulated sandwich panels have transformed the construction of modern cold storage facilities by offering superior thermal insulation, energy efficiency, durability, and fast installation. Their ability to maintain stable temperatures while reducing operational costs makes them an ideal choice for industries that depend on reliable refrigeration systems.
From food storage and pharmaceuticals to logistics and agriculture, insulated sandwich panels provide the performance and reliability required for efficient cold chain operations. As demand for temperature-controlled infrastructure continues to grow, these panels will remain a smart and practical solution for building advanced cold storage facilities.